Computer vision
A real recording, piece by piece.
It detects the pieces, tracks each one with an ID and counts it when it crosses a line. Below, step by step, on a real recording of a breaded-product line.
Anatomy of a count
Hover or tap each step to see where it happens in the image. The event log fills with the events the model recorded on this recording, at the exact frame you're watching.
Status: automatic counting is in validation on the plant floor; its accuracy is measured against a manual count before it's published.
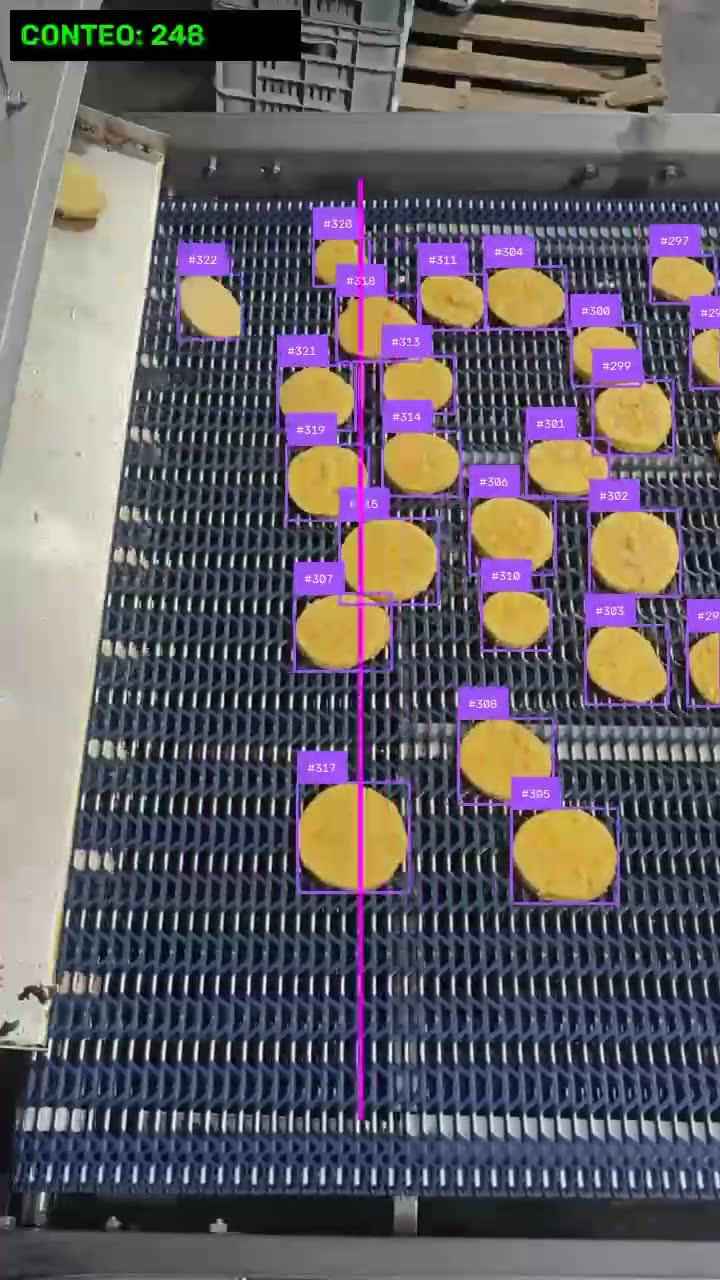
What the model is doing
Event log
Recorded by the model- Play the recording to see the events.
What reaches the platform
Demo data- Order
- OP-DEMO-0142
- Shift
- A · 06:00–14:00
- Product
- Breaded, line 1
- Status
- Running
- Pieces counted
- —
- Pace · last 10 s
- —/min
Count and pace: the model's recorded output on this recording (not an accuracy measurement). Order, product and shift: example.
Why we process in the plant
Video is analysed on a computer next to the line. Only numbers and timestamped events travel to the platform: less bandwidth, no dependence on the internet to count, and the images stay in your plant.
Inside your plant
Camera
on the line
Edge computer
inference next to the line
Autech platform
orders, stops, alerts
Status: processing next to the line is in validation; it is confirmed on each installation.
- Speed
- The “a piece passed” decision is made next to the line, without depending on the internet.
- Bandwidth
- No video is sent anywhere: only numbers and events.
- Privacy
- Images stay in your plant.
- Continuity
- Designed to buffer if the connection drops and sync when it's back.
Calibration: every line is different
- Camera position and height over the belt
- Lens for the distance and width to cover
- Stable lighting, without glare or shadows
- Region of interest and counting-line placement
- Belt speed and spacing between pieces
How we validate a count
- 01
We record your line
With your product, your lighting and your speed: the model is tuned to your case.
- 02
We compare against a manual count
On recordings the model didn't learn from, piece by piece.
- 03
We measure again when something changes
Product, lighting, speed or camera position.
What you get: the agreement between the manual count and the model's, measured on your product and your line, before anyone relies on the number. We don't publish a generic accuracy: it depends on each installation.
A count on its own isn't worth much. In Autech it's linked to the order, line, shift and lot, and feeds dashboards, stops and alerts.
Where it applies
Automated counting
Pieces on the belt, bags at the packaging exit, finished cases or pallets.
See solution →In validation on the plant floor
Counting at different stages
Fryer exit, freezer infeed, packaging: comparing stages shows where product is lost.
See solution →In validation on the plant floor
Flow-based stop detection
If product stops passing in front of the camera, the stop is recorded with its start time.
See solution →In validation on the plant floor
Visual inspection
Shape, size or visible defects. Requires images of your product and criteria defined with quality.
See solution →Where we're heading
Operational monitoring
Pile-ups, gaps on the belt or idle zones, depending on what matters in your process.
Where we're heading
Bring your product. We'll count it on your line.
Tell us what's costing you most today. We review it with you, show how we'd solve it and estimate its value together.